X

Partner Login

Enter your username and password here on order to log in on the partner portal:

No registered partner yet?

Register now

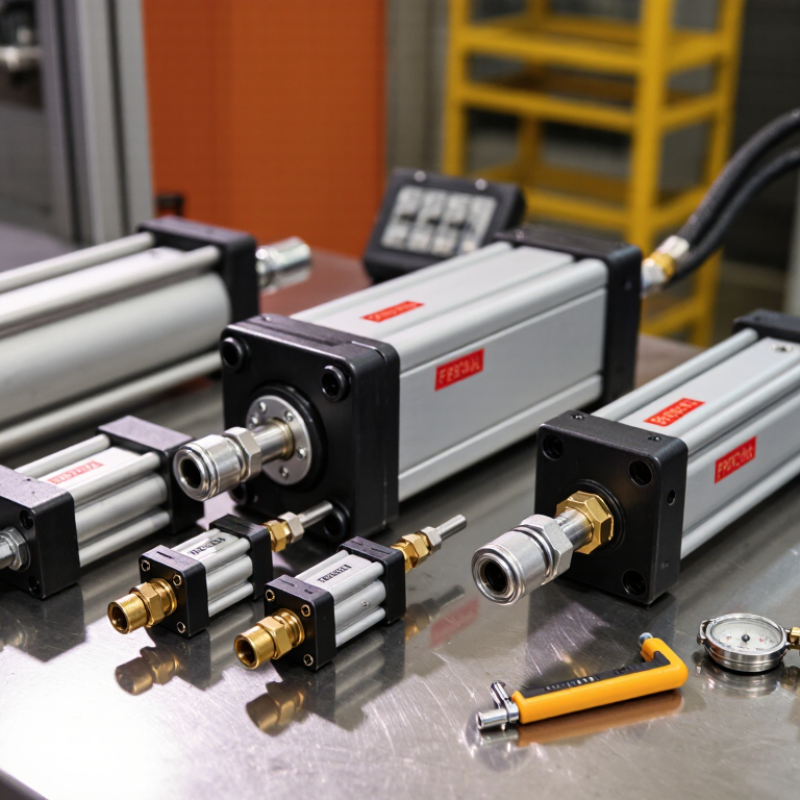
How to Choose the Right Festo Pneumatic Cylinder?

Choosing the right Festo Pneumatic Cylinder is not simply a matter of matching bore size and stroke length. A cylinder may fit the drawing yet fail under real factory conditions. Air pressure changes. Loads move unevenly. Dust collects around the rod seal.

Dr. Frank Melzer, former Chief Technology Officer at Festo, has said, “Digitalisation is not an end in itself; it must create customer value.” That principle also applies to pneumatic selection. The correct Festo Pneumatic Cylinder should solve a measurable motion problem, not merely add an impressive specification. This guide examines load direction, stroke distance, operating pressure, speed control, mounting style, and environmental exposure. It also considers sensors, cushioning, available installation space, and maintenance access.

Small details matter.

For example, a horizontal slide carrying a 12-kilogram fixture needs more than a simple force calculation. Friction, stopping impact, acceleration, and safety margin can change the result. A compact cylinder may work during testing, then hesitate after months of side loading. That uncomfortable possibility deserves attention. Engineers sometimes select the smallest model to reduce cost, but this choice can increase wear and downtime.

The following sections provide a practical selection path based on Festo documentation, workshop experience, and application-focused engineering judgment. Product data should still be checked against the latest manufacturer specifications. No guide replaces testing the cylinder under actual load, pressure, temperature, and cycle conditions. The best decision is usually the one that remains reliable when the machine is no longer new.

How to Choose the Right Festo Pneumatic Cylinder?

Define Load and Force Needs with F = pA at the Standard 6 bar

Choosing a pneumatic cylinder starts with the load, not the catalog. At the standard 6 bar, use F = pA, where pressure is 0.6 N/mm². Calculate piston area with A = πD²/4. A 32 mm bore provides about 482 N theoretically. A 50 mm bore provides approximately 1,178 N. These figures describe extension force before losses. They are not working guarantees.

Rod-side force is lower because the rod reduces effective area. Friction, pressure drop, seals, cushioning, and acceleration also consume force. In practical testing, a cylinder may stall when the calculation looks perfect. That assumption needs checking. Measure the real load, travel speed, mounting position, and cycle frequency. For vertical loads, include gravity and the force needed to start movement. Select a suitable force margin after testing, rather than guessing from bore size alone.

Compressed air quality also affects reliability. The U.S. Department of Energy’s Improving Compressed Air System Performance guidance reports that leaks can waste 20–30% of compressor output. A leaking fitting near the cylinder can therefore reduce available force during demanding cycles. ISO 15552 dimensions help standardize cylinder selection, but they do not replace system verification. Check pressure at the cylinder port while moving, not only at the compressor gauge. Record the lowest reading. Then compare it with the force required at that exact moment.

Match Festo Cylinder Types to ISO 6432 and ISO 15552 Requirements

Choosing the right pneumatic cylinder starts with the mounting standard, not the logo on the cylinder.

ISO 6432 suits compact, round cylinders for light automation, pick-and-place units, and limited spaces. ISO 15552 fits larger profile cylinders with stronger mounting options and higher force potential. Check the available bore sizes, stroke lengths, port positions, and mounting interfaces before selecting a model.

Calculate force from bore area and working pressure, then allow a practical safety margin.

Friction, side loads, speed changes, and pressure losses can reduce actual performance. A 50 mm stroke may look correct on paper, but the mechanism might need extra travel for alignment.

Use a guided carriage when the rod will face bending forces. Never treat the cylinder rod as a guide.

In field installations, cushioning often decides whether a system runs quietly or fails early. Adjustable end cushioning helps control a fast load near the stroke limit.

Confirm the required rod thread, seal material, temperature range, and protection level. ISO compliance does not guarantee suitability for every environment.

A cylinder can meet ISO 15552 dimensions and still perform poorly in dust or washdown conditions.

I have found that dimension drawings deserve more attention than product names. One overlooked mounting gap can force a redesign.

Recheck the full assembly, including brackets, tubing, sensors, and maintenance access, before approval.

Choose Bore and Stroke from Common 32–125 mm ISO 15552 Sizes

Choosing the right pneumatic cylinder begins with two dimensions: bore and stroke. For common ISO 15552 designs, bore sizes from 32 to 125 mm suit many industrial applications. Bore controls pushing force. Stroke controls the required travel distance. That sounds simple, but machine layouts often hide the real limits. Measure movement at the load, not only the available frame space.

At 6 bar, a 32 mm bore produces approximately 480 N of theoretical extension force. A 125 mm bore produces about 7,360 N. Actual force will be lower because of friction, pressure loss, seals, and acceleration demands. The return force is also reduced by the piston rod area.

A practical design should include a sensible force margin, often around 25% to 50%. This margin depends on load variation and operating speed.

Stroke selection needs equal care. A stroke that is too short may stop before the mechanism reaches its position. An unnecessarily long stroke can increase bending risk, vibration, and installation space. Check the rod alignment, mounting support, and side loads.

Add adjustable cushioning when the piston moves a heavy load quickly. Magnetic position sensing may also help with reliable cycle control.

A common field mistake is choosing the largest bore “for safety.” It may work, but it can waste air and create harsh motion. Recheck the force calculation, especially when friction changes during real operation.

Check the 1–10 bar Pressure Range, Speed, and Cushioning Options

Choosing a pneumatic cylinder starts with its working pressure, not its catalog maximum. A 1–10 bar range offers flexibility, but the real operating point matters more. At 1 bar, friction and load resistance may prevent smooth movement. Near 10 bar, seals and mounting parts face greater stress. Calculate force with piston area multiplied by pressure, then allow for friction and safety margin. Use a regulator and gauge beside the cylinder. This makes pressure changes visible during testing. I have seen systems fail because designers trusted nominal pressure without checking actual supply losses.

Speed depends on airflow, tubing length, valve size, load, and pressure. A flow-control valve can help, but adjustment should happen while observing the complete cycle. Meter-out control often gives steadier motion with changing loads. Do not chase maximum speed too early. It can create noise, vibration, and premature wear. Test the cylinder under its real load.

Cushioning controls the final part of the stroke. Adjustable cushions can reduce impact before the piston reaches the end cap. They need careful tuning. Too much restriction causes hesitation; too little creates a sharp удар. Check both extension and retraction, because their loads may differ. Temperature and contamination can also change performance. A short trial on the workbench is useful, but production testing remains necessary.

Verify Mounting, Environment, and Service-Life Requirements Before Selection

Selecting a pneumatic cylinder starts with the mounting arrangement, not the bore size. Confirm the stroke, load direction, available space, and required speed. A clevis mount suits pivoting motion, while a rigid flange mount needs accurate alignment. Side loading is a common mistake. It can accelerate rod, seal, and bearing wear. ISO 15552 dimensions help standardize interchangeability, but they do not correct poor machine alignment.

Environment changes the selection quickly. Check temperature, humidity, dust, chemicals, and washdown frequency. Food-processing areas may require corrosion-resistant materials and suitable sealing compounds. Outdoor equipment may need protection from ultraviolet exposure and freezing moisture. Compressed-air quality matters too. The U.S. Department of Energy’s Improving Compressed Air System Performance guide reports that leaks can waste 20–30% of compressor output. Contaminated air can shorten service life. Small filters are not always enough.

Service life should be calculated from cycles, duty rate, cushioning, and maintenance access. Estimate daily strokes, then compare that figure with endurance data tested under similar conditions. ISO 19973 provides a framework for pneumatic component reliability testing, but laboratory results rarely match every factory. That deserves caution. A cylinder rated for millions of cycles may fail early under side load or poor lubrication. Record cycle counts, inspect rod surfaces, and review failures after installation. The first selection may be wrong. That is useful evidence, not a reason to hide the problem.

How to Choose the Right Festo Pneumatic Cylinder? - Verify Mounting, Environment, and Service-Life Requirements Before Selection
Selection Dimension Typical Requirement or Data What to Verify Before Selection Selection Guidance
1. Load, Force, and Motion Requirements
Required pushing force Determine the external load, friction, acceleration force, and a design margin. Calculate the total required force at the lowest available operating pressure. F = P × A Select a bore that provides more force than the calculated requirement. A practical design margin is commonly added to account for friction, pressure variation, and dynamic effects.
Theoretical force at 6 bar Indicative extension force:
32 mm bore: 483 N
50 mm bore: 1,178 N
63 mm bore: 1,871 N
80 mm bore: 3,016 N
100 mm bore: 4,712 N
Values are calculated from a nominal pressure of 6 bar using the piston area. Actual output is lower because of seal friction, pressure losses, and operating conditions. Use these values for preliminary sizing only. Confirm the manufacturer's force tables and the actual working pressure before final selection.
Retracting force Retracting force is lower than extending force because the rod occupies part of the piston area. Use: Fretract = P × (Apiston − Arod) Size the cylinder using the weaker direction if the application requires equal performance in both directions.
Stroke length The travel needed to complete the machine movement, plus any required clearance. Measure the actual end-to-end travel and check whether the load must stop before the mechanical end of the cylinder. Choose the shortest standard stroke that meets the movement requirement. Excessive stroke can increase deflection, bending risk, and installation space.
Operating speed Required cycle time and average rod speed. Estimate: Speed = Stroke ÷ Time
Check available air flow, tubing length, valve capacity, load inertia, and cushioning requirements.
Use flow controls and suitable valve sizing. Avoid relying on pressure regulation alone to control speed.
Cycle frequency Number of extend-and-retract cycles per minute or per hour. Record the duty cycle, idle periods, stroke length, speed, load, and end-position impact. Select a cylinder rated for the required duty and confirm seal, guide, and cushioning suitability for continuous operation.
2. Mounting and Mechanical Alignment
Mounting style Fixed, pivoting, trunnion, flange, foot, clevis, or other mounting arrangement. Compare the available machine interfaces with the cylinder mounting dimensions, fastener locations, and required articulation. Use fixed mounts for accurately aligned loads. Use pivoting or clevis arrangements where the load angle changes during the stroke.
Rod-side alignment The rod should transmit axial force without side loading. Check parallelism between the cylinder centerline and the guided load. Inspect the complete motion path for angular misalignment. Add an external guide, spherical joint, or guided cylinder where the load can create lateral force or bending moment.
Side load and bending Side loads should be minimized because they accelerate rod, bearing, and seal wear. Evaluate load offset, unsupported rod length, impact forces, and the distance between the cylinder mount and the load center. Increase rod diameter or use external guidance only after confirming the mechanical design. Do not use the cylinder rod as a structural guide unless it is specifically designed for that purpose.
End-position impact The moving mass must decelerate before reaching the stroke end. Check moving mass, speed, pressure, cycle rate, and whether the cylinder has adjustable or fixed cushioning. Choose adjustable cushioning for variable loads or speeds. Use external shock absorbers when the impact energy exceeds the cylinder's cushioning capability.
3. Operating Environment
Operating pressure Common industrial compressed-air systems operate around 5 to 7 bar, but the actual pressure depends on the installation. Measure pressure at the cylinder inlet during the fastest and highest-load part of the cycle, not only at the compressor or manifold. Confirm that the cylinder's permitted pressure range covers the minimum and maximum pressure, including temporary peaks.
Temperature Ambient and process temperatures may vary during production. Record minimum, normal, and maximum temperatures near the cylinder, including heat from ovens, motors, sunlight, and washdown. Select seals, lubricants, and materials rated for the full temperature range. Do not assume standard seals are suitable for high or low temperatures.
Water, dust, and chemicals Exposure may include humidity, washdown, abrasive dust, oil mist, cleaning agents, or corrosive vapors. Identify the type, concentration, frequency, and temperature of each contaminant. Specify appropriate corrosion-resistant materials, rod protection, wipers, seals, and ingress protection for the environment.
Clean or hygienic area Applications may require low particle generation, clean materials, or frequent sanitation. Check applicable hygiene, cleanroom, food-contact, or contamination-control requirements. Select a cylinder construction and lubricant approved for the relevant application. Confirm compatibility with cleaning chemicals and sanitation temperature.
Compressed-air quality Air quality affects seal life, corrosion, valve performance, and reliability. Check filtration, water separation, oil content, dew point, and the requirements of the complete pneumatic system. Use suitable air preparation and avoid excessive oil or water carryover. Follow the cylinder manufacturer's lubrication requirements.
4. Service Life, Maintenance, and Safety
Expected service life Define the required number of cycles, operating hours, and maintenance interval. Document cycle rate, stroke, load, speed, pressure, temperature, side load, and end-position impact. Choose a design with adequate guide capacity, seal compatibility, cushioning, and load margin. Service life cannot be predicted from cycle count alone.
Maintenance access Routine inspection and replacement should be possible without excessive machine downtime. Check access to ports, fittings, sensors, fasteners, seals, and mounting hardware. Provide space for inspection, rod cleaning, leak checks, and replacement. Consider modular or repairable designs where downtime is critical.
Position sensing The control system may need confirmation of retracted, extended, or intermediate positions. Determine sensor type, switching distance, electrical supply, connector location, and environmental protection. Select compatible magnetic or external position sensing and verify that the sensor remains reliable at the required speed and temperature.
Failure and safety behavior Loss of air or electrical power may cause unexpected movement or load release. Perform a risk assessment covering stored air energy, gravity loads, pinch points, unexpected restart, and pressure loss. Add mechanical restraints, locking devices, exhaust valves, flow controls, guarding, or other safety measures where required. A pneumatic cylinder alone should not be treated as a safety lock.
Final selection record Bore, stroke, rod diameter, mounting, ports, cushioning, seals, sensors, pressure range, temperature range, and materials. Compare the completed specification with the machine drawing, pneumatic schematic, risk assessment, and maintenance plan. Approve the cylinder only after all mechanical, pneumatic, environmental, service-life, and safety requirements have been verified together.
Important calculation note Theoretical force is based on pressure multiplied by effective piston area. Real available force is affected by seal friction, pressure drop, flow restrictions, acceleration, load geometry, leakage, temperature, and alignment. Always validate the final choice under representative operating conditions.